Vision Systems for Manufacturing: A Complete Guide
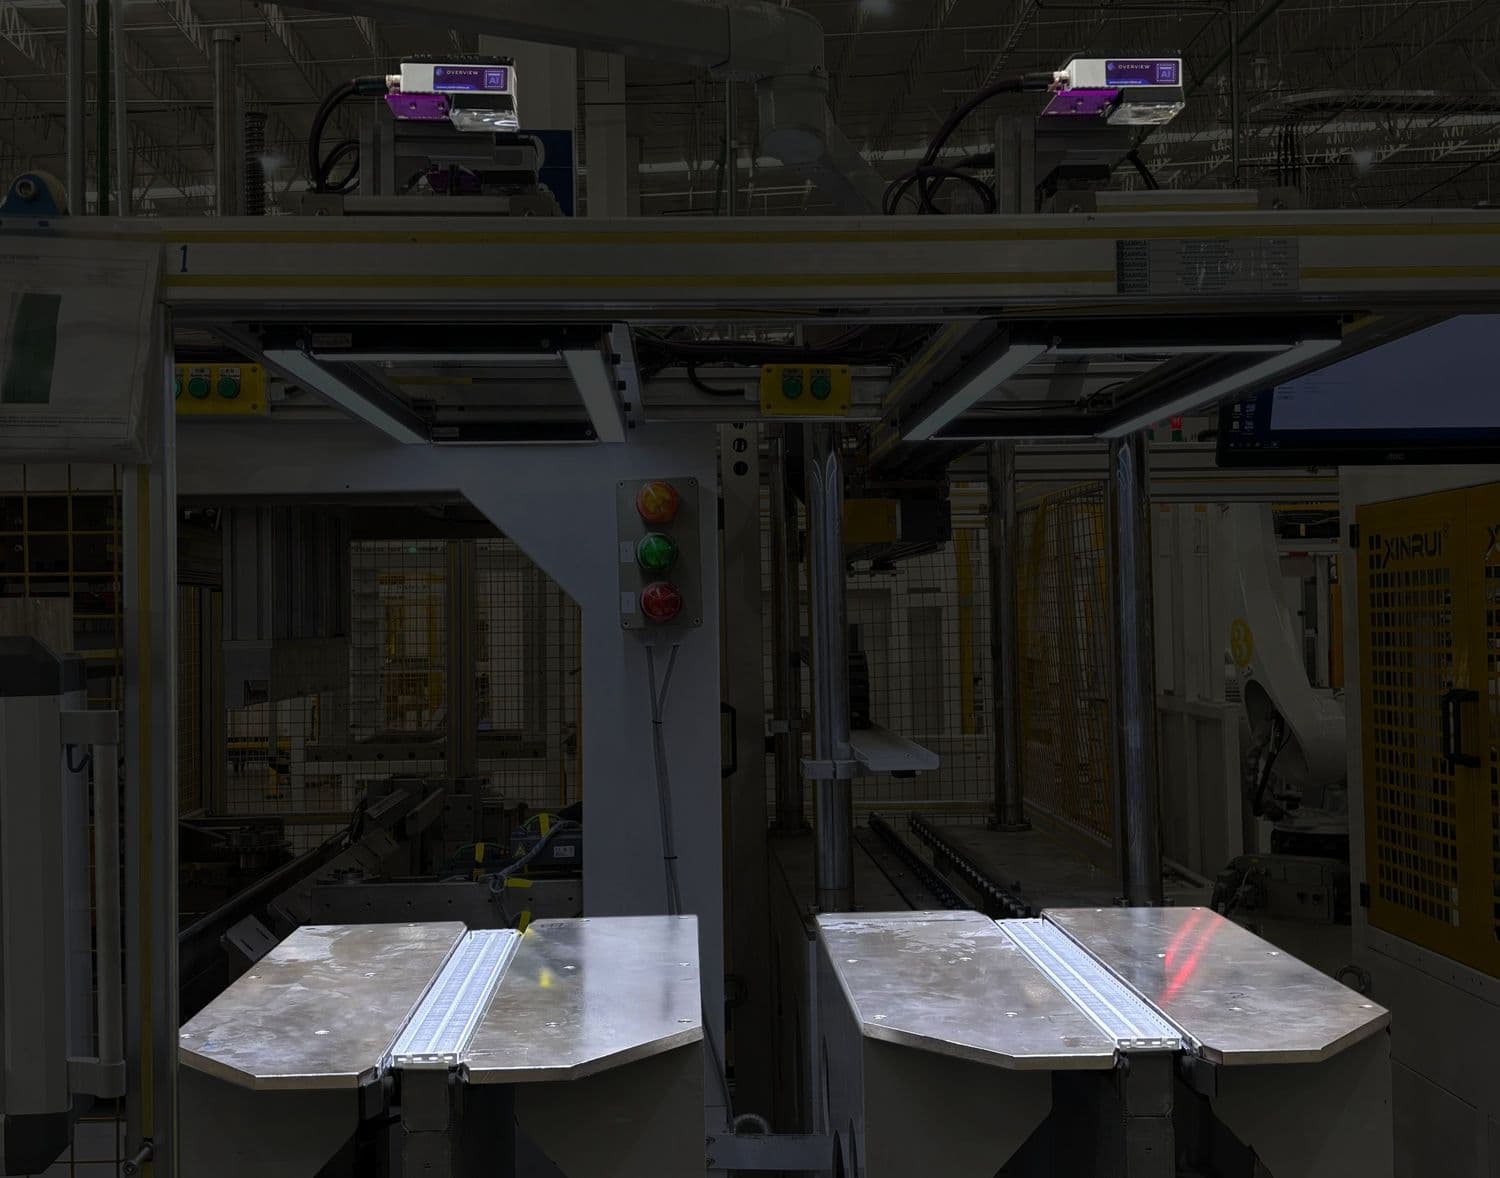
A vision system is an integrated combination of cameras, lighting, optics, processing hardware and software that captures images of a product and turns them into a decision or a measurement.
This guide covers the components and how to choose between them. For the system-level view, the main types and how they work step by step, see machine vision systems.
Vision systems have become indispensable in modern manufacturing. From simple presence detection to complex quality inspection, these systems use cameras and image processing to automate visual tasks that once required human eyes. This guide provides a comprehensive overview of vision systems for manufacturing professionals.
What Is a Vision System?
A vision system is an integrated combination of hardware and software that captures and analyzes images to make decisions or measurements. In manufacturing, vision systems inspect products, guide robots, read codes, measure dimensions, and verify assembly, tasks that require "seeing" and interpreting visual information.
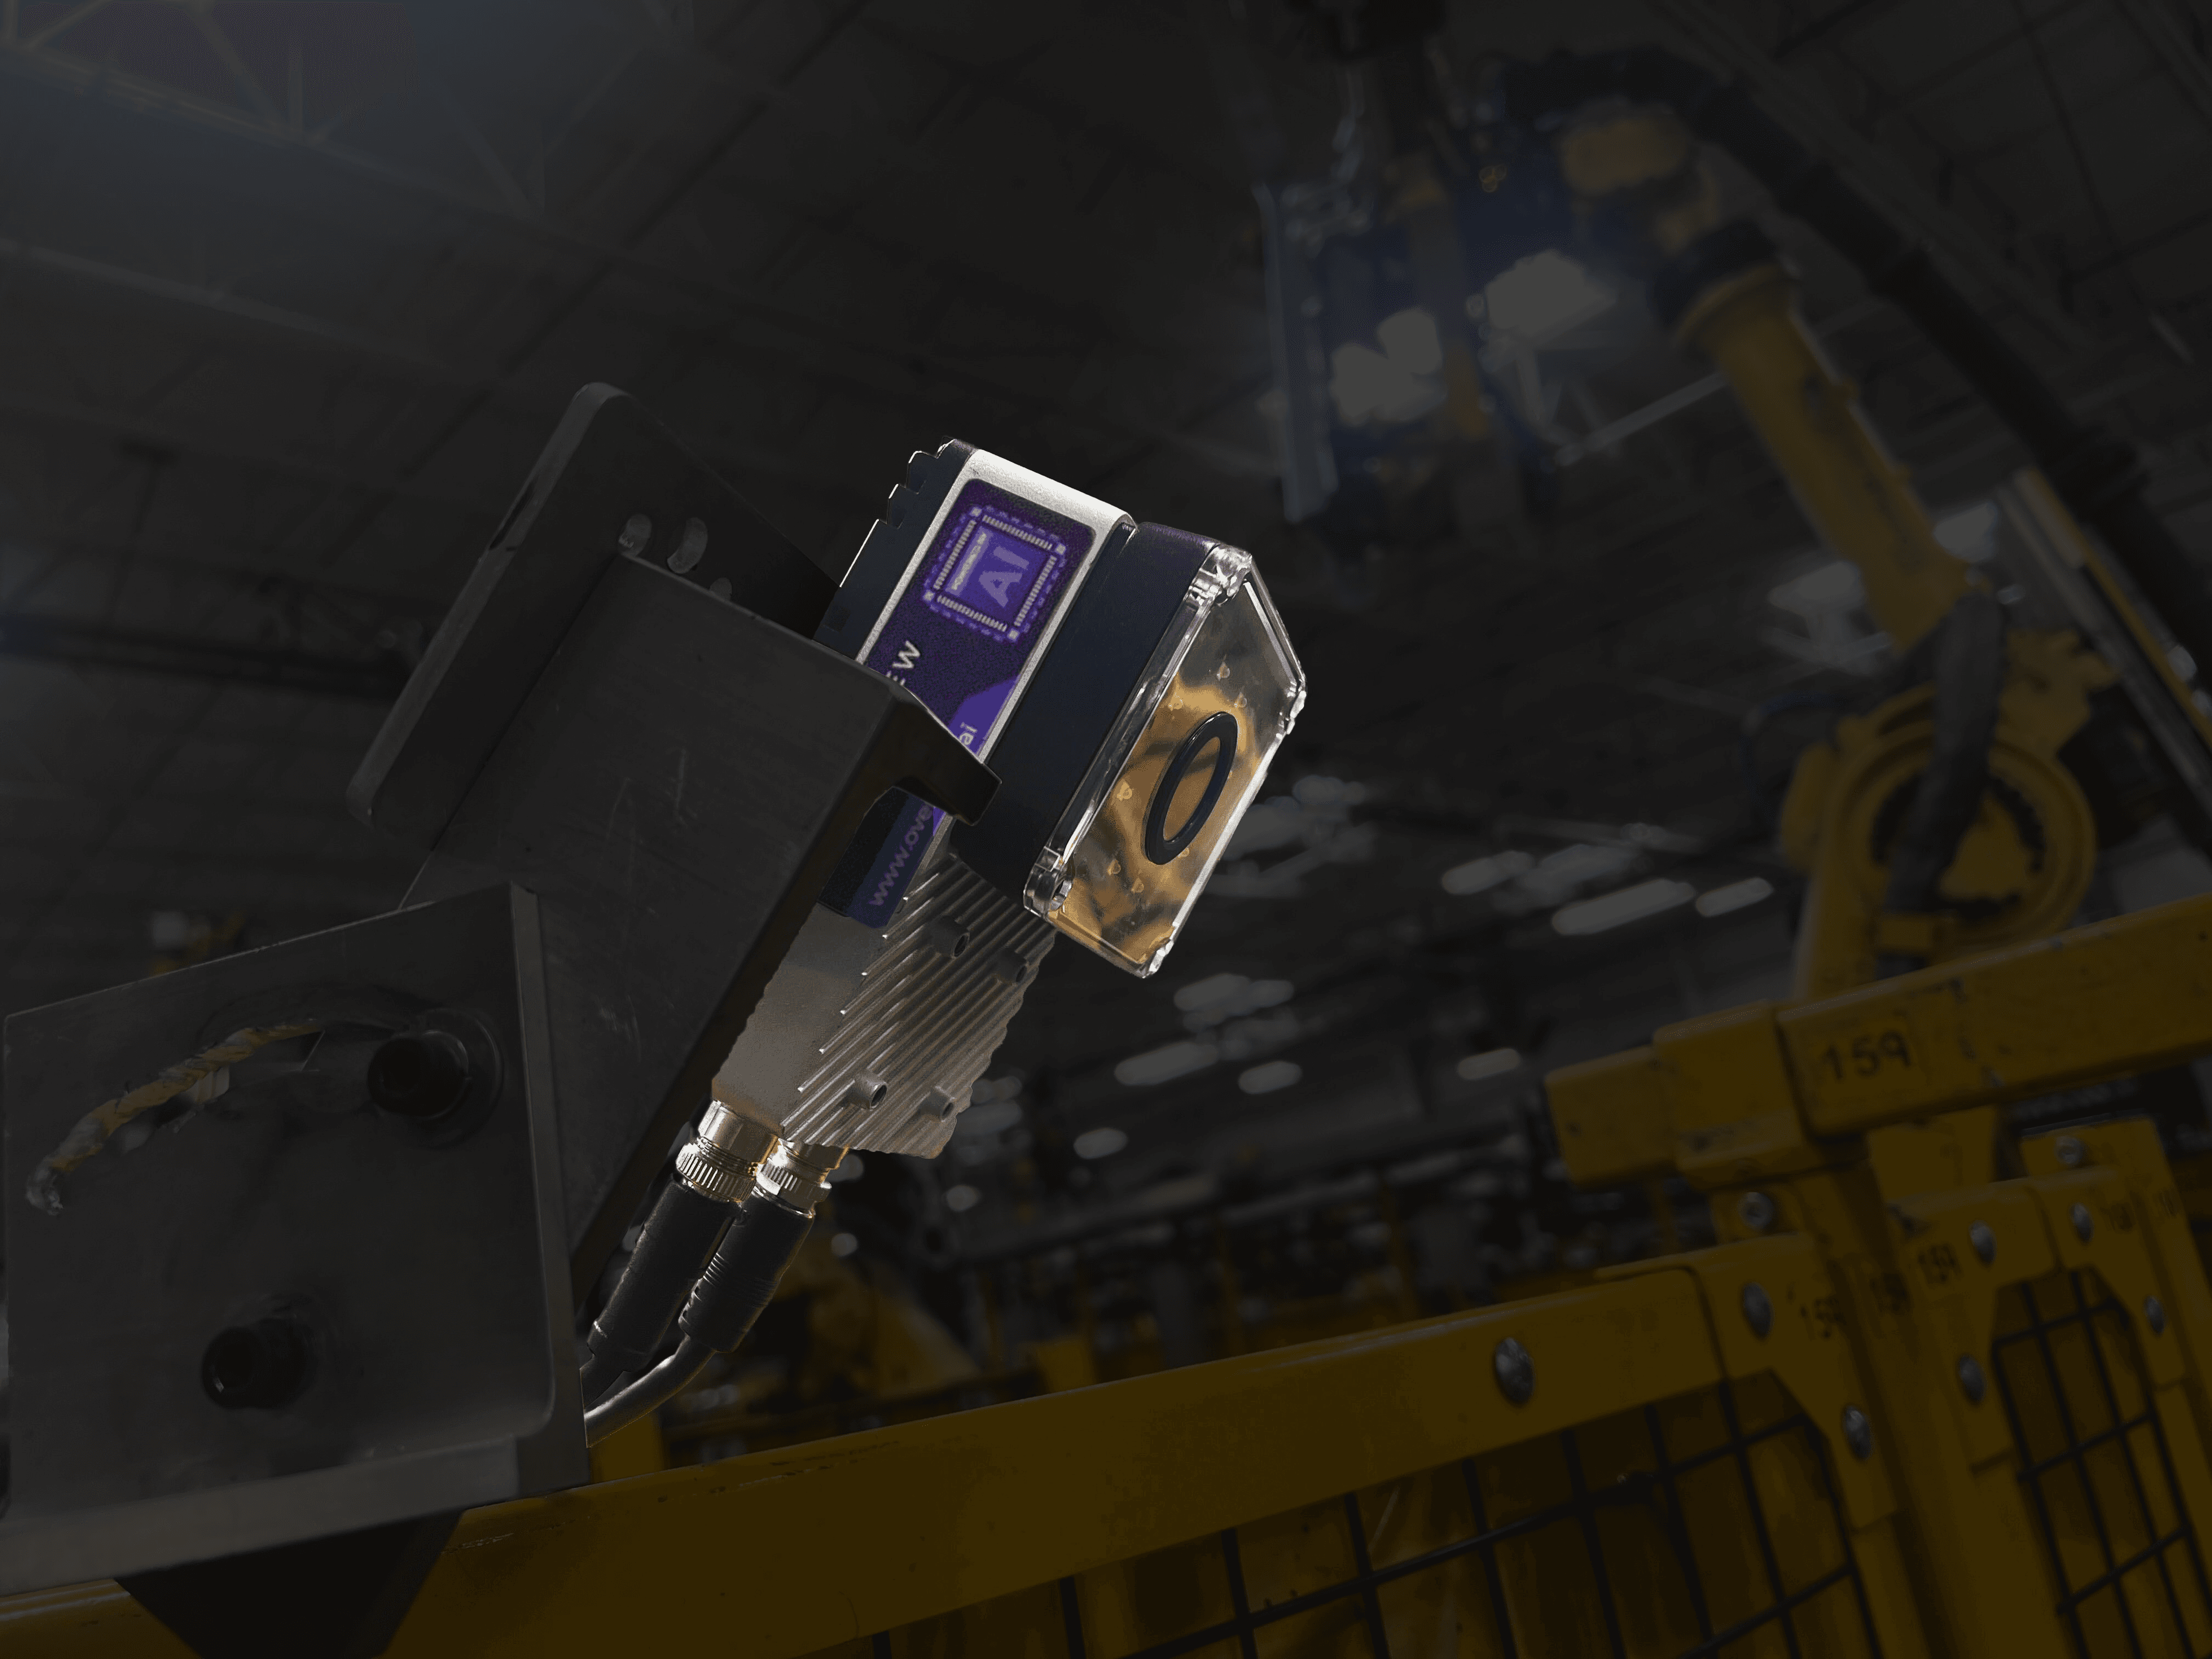
Unlike human vision, which is subjective and prone to fatigue, vision systems provide objective, consistent, and tireless visual analysis. They can inspect products at speeds impossible for humans, operate continuously without breaks, and apply identical criteria to every inspection.
Core Components of a Vision System
Cameras
The camera is the "eye" of the vision system, capturing images of products for analysis. Industrial cameras differ significantly from consumer cameras; they're built for reliability, precise triggering, and integration with industrial systems. Their measured performance is stated against EMVA 1288, and they present a common programming interface through GenICam, which is what lets one vendor’s software drive another vendor’s camera.
Area Scan Cameras
What it is: Capture a complete 2D image in a single exposure.
Best for: Discrete parts that can be positioned in the field of view at a station.
Line Scan Cameras
What it is: Capture one row of pixels at a time and build the image from the product's motion.
Best for: Continuous web, sheet, strip and cylindrical products, where there is no natural part boundary.
3D Cameras
What it is: Capture depth alongside the 2D image, from structured light, stereo or laser triangulation.
Best for: Height, volume, warpage and seating checks that a flat image cannot answer.
Smart Cameras
What it is: Integrate the camera, processor and inspection software in one housing.
Best for: Standalone inspection where you want one unit to mount rather than a rig to specify.
Lighting
Lighting is arguably the most critical component of a vision system. Proper lighting reveals the features you need to inspect while minimizing features that could confuse analysis. Poor lighting makes reliable inspection impossible regardless of camera or software quality.
Common Lighting Techniques:
- Front lighting: Illuminates surface features, good for color and texture inspection
- Backlighting: Silhouettes objects against bright background, ideal for edge detection and dimensional measurement
- Diffuse lighting: Soft, even illumination that minimizes glare on reflective surfaces
- Structured lighting: Projects patterns onto surfaces to reveal 3D shape and surface defects
- Dark field lighting: Low-angle illumination that highlights surface scratches and defects
Optics
What it does: The lens focuses light onto the sensor and fixes the field of view, the working distance and how much detail lands on each pixel.
Why it matters: Optics cap what the system can resolve, so no amount of processing recovers a defect the lens never imaged.
Processing Hardware
What it does: The processor runs the analysis, from an embedded chip inside a smart camera to an industrial PC driving several cameras.
Why it matters: Available compute sets how fast each image can be analysed, which is what decides your maximum line speed.
Software
The transport standards those images travel over, GigE Vision and USB3 Vision, are maintained by A3.
What it does: The software turns the image into a result, either with programmed algorithms such as edge detection, pattern matching and blob analysis, or with a trained model.
Why it matters: Programmed algorithms are exact where the tolerance is numeric. A trained model is what makes variable surfaces and cosmetic defects practical to automate.
Manufacturing Applications
Quality Inspection
The most common application: examining products for defects. Vision systems detect surface flaws, verify color and appearance, check for contamination, and identify damaged products. Inspection can be simple (is the cap present?) or complex (are there any scratches on this automotive panel?). Explore surface inspection applications.
Measurement and Gauging
Vision systems measure product dimensions without physical contact. They verify lengths, widths, diameters, angles, and positions. Non-contact measurement is faster than manual gauging and doesn't risk damaging delicate products.
Identification and Tracking
Reading barcodes, QR codes, data matrix codes, and OCR (optical character recognition) enables product tracking and traceability. Vision systems read codes at high speeds, even when damaged or poorly printed, and verify that correct information is printed.
Robot Guidance
Vision-guided robotics uses cameras to locate parts and guide robot movements. Instead of requiring parts in precise positions, robots can find and pick parts from varying locations, enabling more flexible automation.
Assembly Verification
Verifying that assemblies are complete and correct, with all components present, properly positioned, and correctly oriented. Assembly verification catches errors before products ship to customers.
Selecting a Vision System
Choosing the right vision system requires matching capabilities to application requirements:
Key Selection Criteria:
- Resolution requirements: What's the smallest feature you need to detect or measure? This drives camera resolution and optics selection.
- Speed requirements: How fast must inspection occur? This affects camera type, exposure time, and processing power.
- Field of view: How large an area must be inspected? Determines lens selection and potentially need for multiple cameras.
- Environment: Temperature, vibration, contamination, and other environmental factors affect component selection.
- Integration: How will the system communicate with other equipment? Industrial protocols, I/O, and data interfaces matter.
- Ease of use: Who will set up and maintain the system? This affects software and platform selection.
System Architectures
Smart Camera Systems
Self-contained units with camera, processor, and software in one package. Easy to deploy for single-point inspection tasks. Limited by the processing power and flexibility that can fit in a compact form factor.
PC-Based Systems

Separate cameras connected to industrial PCs running vision software. More flexible and powerful than smart cameras. Can handle multiple cameras and complex processing. Requires more integration effort.
Integrated Systems
Purpose-built systems that combine camera, processing, software, and sometimes lighting into tested, supported packages. Simplify deployment by eliminating component selection and integration. Trade some flexibility for ease of implementation.
Implementation Best Practices
- Start with lighting: Get lighting right before worrying about cameras or software. Most vision problems are actually lighting problems.
- Define clear requirements: What exactly must be detected or measured? What speeds are required? What accuracy is needed?
- Test with real samples: Use actual production parts, including the full range of acceptable variation and known defects.
- Plan for maintenance: Vision systems need ongoing attention. Plan for cleaning, calibration, and adjustment.
- Consider total cost: Include integration, training, and maintenance, not just hardware purchase price.
- Involve operators: The people who will use and maintain the system should be involved in selection and implementation.
The Evolution of Vision Systems
Vision systems continue to evolve rapidly. Traditional rule-based systems are being augmented and sometimes replaced by learning-based approaches that can handle more complex, variable inspection tasks. Processing power continues to increase while costs decrease. Cameras offer higher resolution and faster speeds. Integration becomes simpler with standardized interfaces.
Modern vision platforms like those from Overview.ai combine the latest imaging technology with advanced processing in integrated packages designed for manufacturing. These systems simplify deployment while delivering capabilities that would have required custom engineering just a few years ago.
Explore Vision System Solutions
See how modern vision systems can address your manufacturing inspection challenges with a personalized demonstration.
Request a DemoFrequently Asked Questions
What is a vision system?
A vision system is an integrated combination of hardware and software that captures and analyzes images to make decisions or measurements. In manufacturing, vision systems inspect products, guide robots, read codes, measure dimensions, and verify assembly, providing objective, consistent, and tireless visual analysis.
What are the core components of a vision system?
A vision system is built from cameras that capture images, lighting that reveals the features being inspected, optics that focus light and set field of view and resolution, processing hardware that analyzes images, and software that extracts information and makes decisions.
Why is lighting so important in a vision system?
Lighting is arguably the most critical component. Proper lighting reveals the features you need to inspect while minimizing features that could confuse analysis, and poor lighting makes reliable inspection impossible regardless of camera or software quality. Most vision problems are actually lighting problems.
How do I choose the right vision system?
Match capabilities to application requirements by considering resolution requirements (the smallest feature you must detect), speed requirements, field of view, the operating environment, integration needs, and ease of use for the people who will set up and maintain the system.
See Overview AI on your parts
Send us a photo of your part or defect and a vision engineer will tell you whether Overview can catch it, with most systems deployed on the line in days.
Related Articles
Computer Vision Solutions for Manufacturing: Finding the Right Fit
How to navigate the landscape of vision options and match the right solution to your products, volumes, and quality challenges.
Read More →Vision AI in Manufacturing: A Practical Introduction
What Vision AI actually does, how it works, key capabilities, and how manufacturers are using it to solve real inspection problems.
Read More →AI Vision Systems Explained: How They Work and What to Look For
How AI vision systems learn from examples, and the capabilities to evaluate when selecting one.
Read More →